The Operational Challenges Manufacturers Face Every Day
If you manage a processing plant, water-treatment system or industrial facility, these challenges are not theoretical. They are daily realities that can affect product quality, equipment performance, process efficiency and operating costs.
The real challenge is not simply having the right chemical. It is having the right chemistry, application approach and technical understanding working together to address the problem effectively.
Because every process is different.
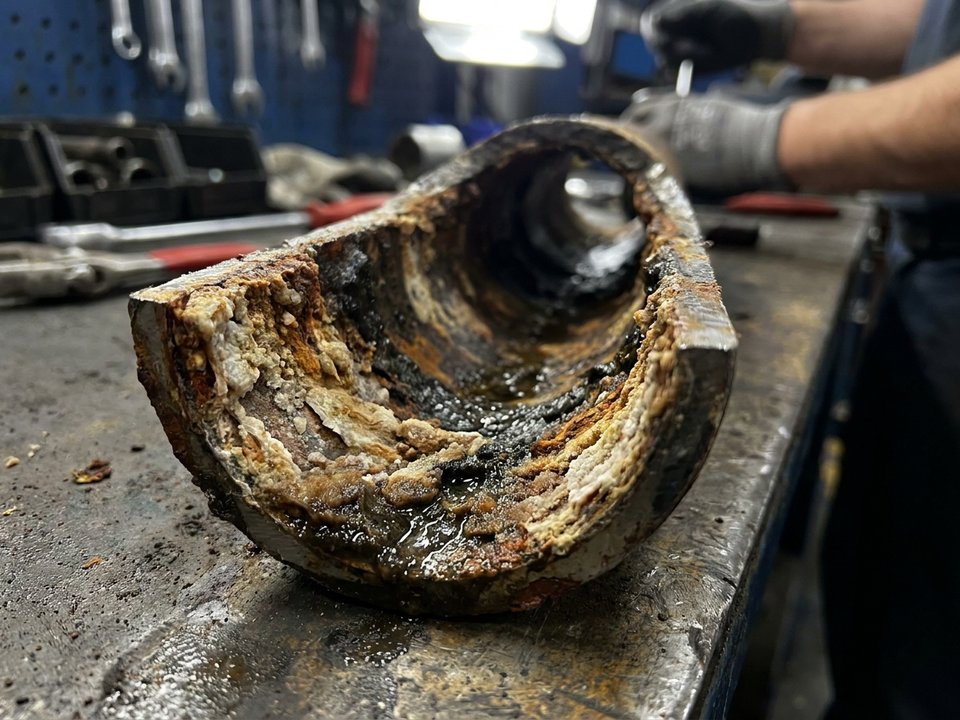
Residue Buildup and Inefficient Cleaning
Product residues can accumulate on plant surfaces, equipment internals and difficult-to-clean areas. When cleaning chemistry is not matched to the soil type, concentration, temperature, contact time and mechanical action, residues may remain, leading to longer cleaning cycles, higher chemical and water consumption and increased hygiene risk.
Microbial Growth and Food-Safety Risk
Inadequate cleaning and sanitation can create conditions that support microbial growth on surfaces, within pipework and across process environments. In food, dairy and beverage operations, inadequate microbial control can increase hygiene risks, compromise product quality and contribute to food-safety concerns.
Production Downtime and Yield Losses
Cleaning failures, fouled systems, equipment issues and extended maintenance can disrupt production schedules and reduce operational availability. Unplanned downtime, longer cleaning cycles and process losses can accumulate into significant production and operating costs.
Membrane Fouling and Performance Loss
Membrane fouling can restrict permeate flow, increase operating pressure requirements and reduce membrane performance over time. Without the right cleaning and conditioning chemistry, fouling can increase cleaning frequency, reduce membrane life and contribute to premature membrane replacement.
Scale Formation and Corrosion
Scale formation and corrosion can affect cooling systems, boilers, water-treatment systems and process equipment. Deposits can reduce heat-transfer efficiency and restrict flow, while corrosion accelerates equipment deterioration, increases maintenance requirements and affects system reliability.
Boiler Sludge and Energy Inefficiency
Sludge and scale accumulation inside boiler systems can reduce heat-transfer efficiency, increase fuel consumption and contribute to under-deposit corrosion and equipment deterioration. Poor boiler-water management can increase operating and maintenance costs while reducing system reliability.
Wastewater Treatment and Regulatory Compliance
Industrial effluent must be treated to meet the applicable discharge requirements and regulatory standards. Inadequate treatment can contribute to elevated pollutant loads, process instability and increased compliance risk, with associated financial and operational consequences.
Application-Focused Chemistry. Not a Catalogue. A Partnership.
We don't start with a chemical. We start with your process.
Every process has its own operating conditions, performance challenges and constraints. A product that works well in one application may not deliver the same result in another.
At Brykonchem, we look beyond the chemical itself. We understand the application, identify the performance challenge and develop the right chemistry and application approach around your process.
Our focus is not simply on supplying chemicals. It is on helping customers achieve more reliable cleaning, better process performance and controlled operating costs through the right technical solution.
Chemistry designed around your process. Performance designed around your needs.
A Structured Approach to Process Performance
At Brykonchem, every engagement follows a structured problem-solving approach. We first understand the application, identify the factors affecting performance and then develop, implement and refine the right chemistry and application approach for your operating conditions.
The objective is simple: achieve reliable performance, improve process efficiency and create measurable operational value.
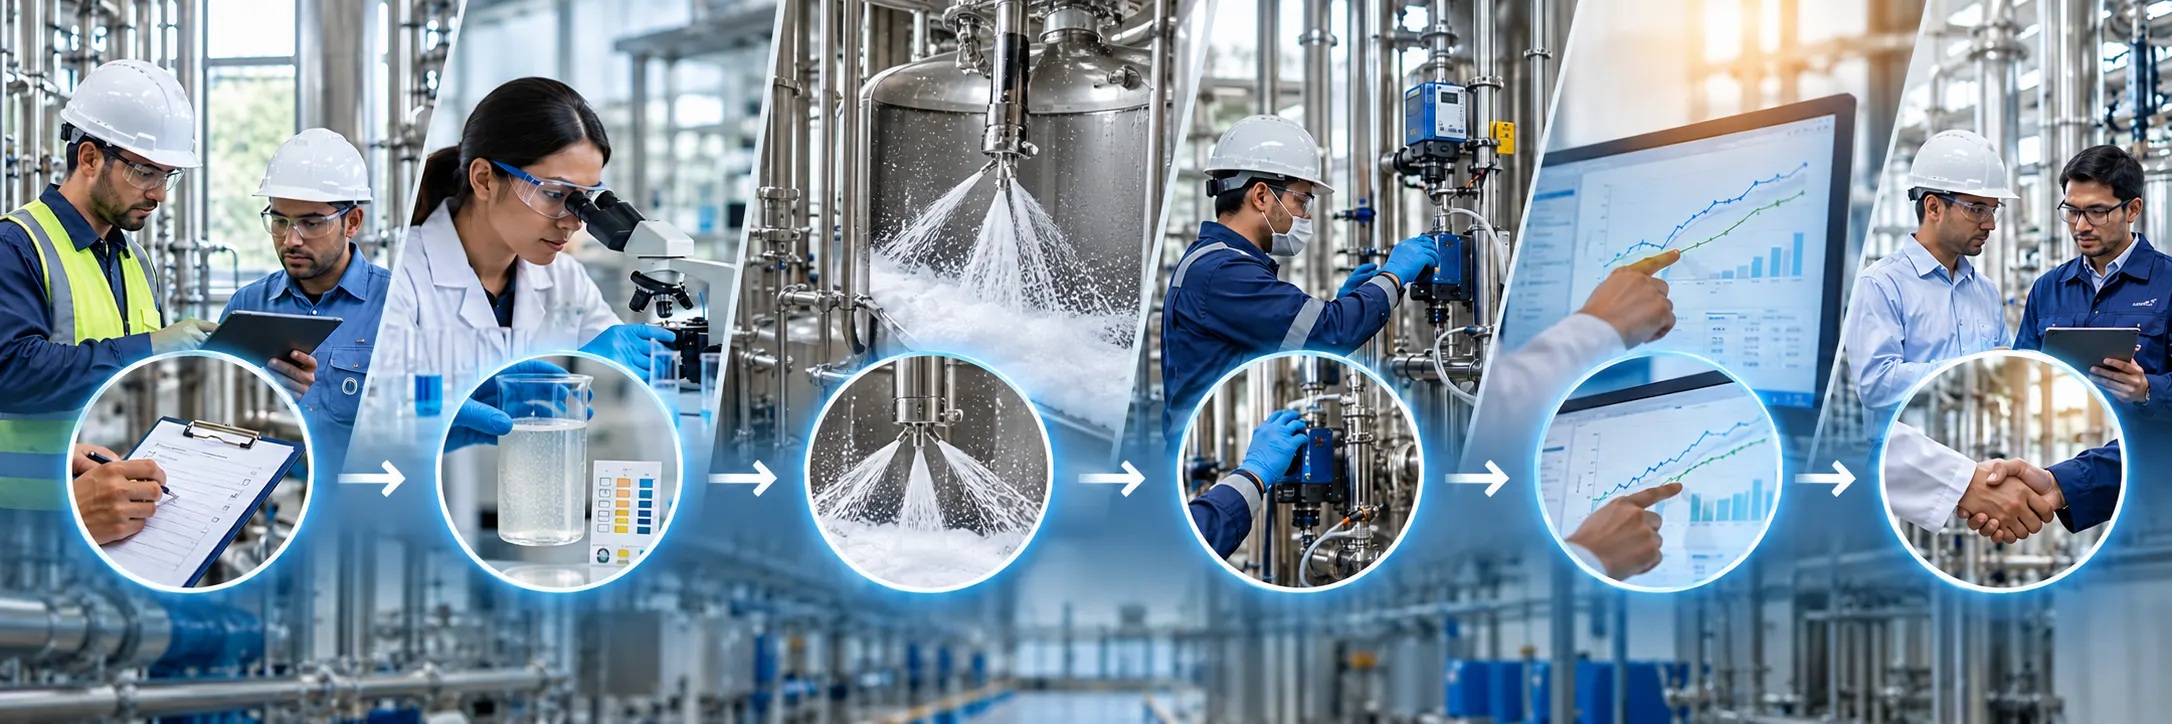
Understand
Start with your process, not the product.
We understand your equipment, operating conditions, existing process, current chemistry and the performance outcomes you need to achieve.
Analyse
Identify what is driving the challenge.
We examine the key factors affecting performance — including soil or foulant type, water quality, temperature, concentration, contact time, mechanical action and existing chemistry.
Recommend
Develop the right chemistry and application approach.
Based on our analysis, we recommend a solution matched to your actual process conditions — rather than simply selecting a product from a standard range.
Implement
Make sure the solution works in practice.
We support correct application, including concentration, dosing, contact time, sequence and process integration, to ensure the recommended approach is implemented correctly from the outset.
Optimize
Improve performance beyond the initial solution.
We evaluate results and refine the approach where required, identifying opportunities to improve cleaning efficiency, reduce chemical or water consumption, improve system performance and extend equipment or membrane life.
Support
Stay involved beyond the initial implementation.
Our technical support continues as your operations evolve — helping with troubleshooting, process changes, performance improvements and new operational challenges.
From Process Understanding to Performance Improvement
We don't just supply chemistry. We work with you to make it perform.
Solutions Across Every Critical Process Area
Brykonchem provides application-focused chemistry and technical support across eight solution areas — each designed around the specific process challenges and performance demands of industrial manufacturing environments.
Clean-in-Place (CIP) Solutions
Residue buildup and inefficient cleaning cycles increase chemical use, water consumption and hygiene risk. Our CIP chemistry is matched to your soil type, equipment and cleaning parameters for consistent, reliable results.
Learn moreMembrane Performance Solutions
Fouling reduces permeate flow and forces operating pressures higher. Our membrane chemistry and application protocols help restore and protect membrane performance to support sustained process efficiency.
Learn moreCooling Water Performance Solutions
Scale, corrosion and microbial growth in cooling systems reduce heat-transfer efficiency and accelerate equipment deterioration. Our approach addresses all three simultaneously.
Learn moreBoiler Reliability Solutions
Sludge, scale and corrosion inside boiler systems reduce efficiency, raise fuel costs and shorten equipment life. Our formulations support reliable boiler operation and controlled maintenance requirements.
Learn moreEffluent Water Treatment Solutions
Industrial wastewater must meet discharge standards. Our application-focused effluent chemistry helps industrial facilities manage treatment effectively and maintain regulatory compliance.
Learn moreHygiene & Sanitation Solutions
Microbial growth on surfaces and in process environments creates food-safety risk. Our hygiene chemistry addresses surface disinfection, hand hygiene and sanitation across food, dairy, beverage and facility environments.
Learn moreRO Membrane Solutions
Declining permeate flow and rising operating pressure signal RO membrane fouling. Our RO-specific chemistry supports cleaning, conditioning and protection of reverse osmosis systems across industrial applications.
Learn moreCustom Formulations
Where standard chemistries do not fit, we evaluate your process conditions, equipment, water characteristics and sustainability objectives to develop or source a formulation tailored to your requirements.
Learn more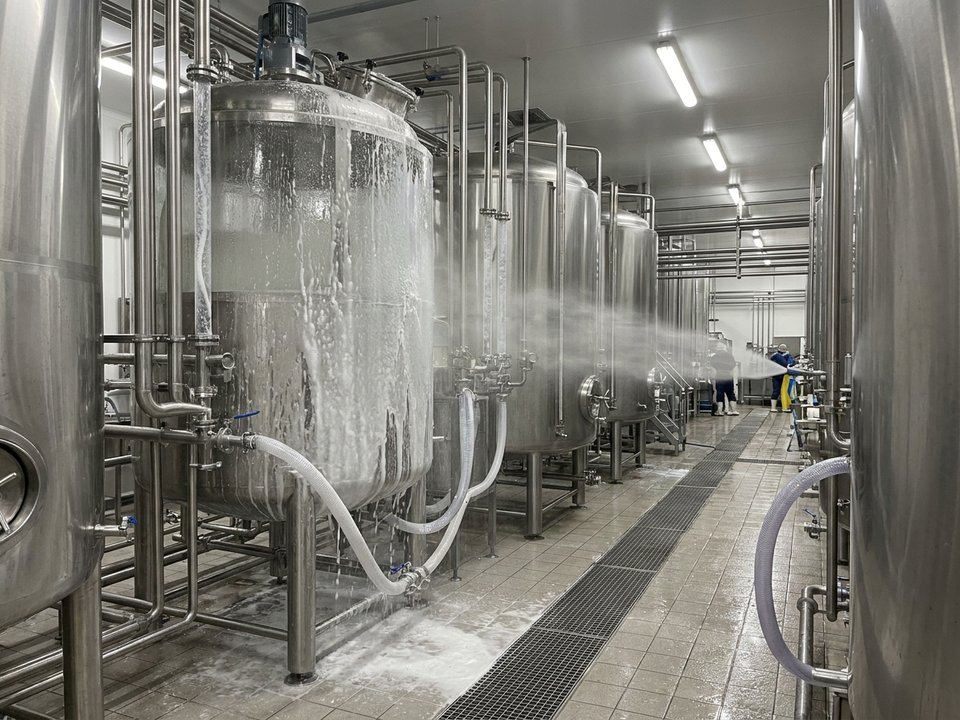
Clean-in-Place (CIP) Solutions
In food, dairy and beverage manufacturing, cleaning is not a support function. It is a production-critical activity. When CIP chemistry is not correctly matched to the process, the consequences compound quickly: residue builds up on heat-exchanger surfaces, pipework and tank walls; cleaning cycles extend to compensate; chemical and water consumption rises; and hygiene assurance weakens even as the cost of cleaning increases.
The root cause in most cases is not insufficient cleaning time or more chemical volume. It is a mismatch between the chemistry and the actual conditions of the application — soil type, process temperature, water hardness, equipment design and mechanical parameters.
Brykonchem's CIP approach starts with identifying exactly what needs to be removed and under what constraints. Proteinaceous soils, fat deposits, mineral scale and combined fouling each respond to different chemical mechanisms, different concentration profiles and different temperature and contact-time requirements. We select and, where necessary, tailor CIP formulations — alkaline cleaners, acid formulations, enzymatic chemistry and combined programmes — to deliver consistent cleaning performance at the lowest practical chemical and water usage.
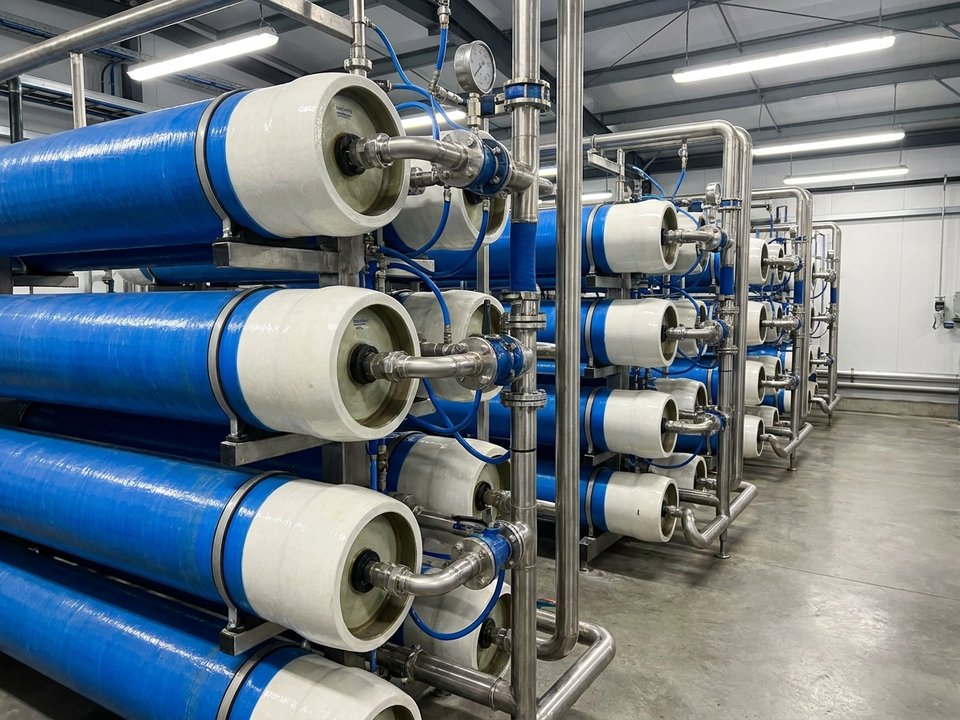
Membrane Performance Solutions
Membrane systems — including reverse osmosis, ultrafiltration and nanofiltration installations — are sensitive to the composition of the water and process streams passing through them. Fouling is not a question of whether it will occur, but of how rapidly and what form it takes. Biological fouling, colloidal deposits, mineral scaling and organic fouling all degrade membrane performance through different mechanisms, and each requires a different chemical response.
The operational signs are consistent regardless of foulant type: permeate flow declines, differential pressure rises, product quality becomes harder to maintain and energy consumption increases. Left unaddressed, membrane integrity deteriorates and replacement intervals shorten.
Brykonchem applies a diagnostic approach to membrane performance challenges. We examine the feed-water characteristics, the fouling pattern, the operating history and the cleaning protocol in use. From this, we recommend a cleaning and conditioning programme matched to the specific fouling mechanism. We also address pre-treatment chemistry and antiscalant dosing as part of an integrated membrane protection strategy.
Cooling Water Performance Solutions
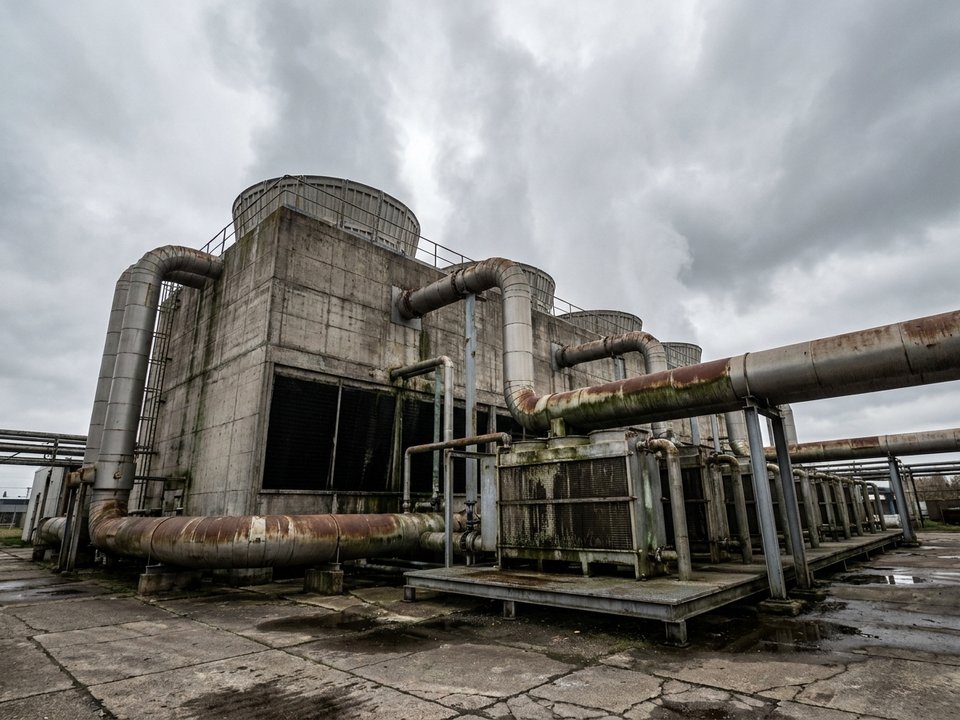
Cooling systems operate under conditions that encourage three distinct and interconnected problems: scale deposition from dissolved minerals concentrating as water evaporates, corrosion from the electrochemical interaction between water, oxygen and metal surfaces, and microbial growth in the warm, circulating water environment. All three reduce system performance and increase maintenance requirements.
Scale on heat-exchanger surfaces acts as an insulating layer, reducing heat-transfer efficiency and forcing systems to work harder to maintain the required temperature differential. Corrosion creates localised metal loss, pitting and ultimately equipment failure. Microbial growth — including biofilm formation — compounds both scaling and corrosion.
Brykonchem's cooling-water programme addresses all three mechanisms through an integrated chemistry and monitoring approach. Scale inhibitors control mineral deposition. Corrosion inhibitors protect metal surfaces across the range of metals typically present in cooling circuits. Biocides and biodispersants control microbial populations and prevent biofilm accumulation. The programme is calibrated to the system's water quality, operating temperature range, cycles of concentration and metallurgy.
Boiler Reliability Solutions
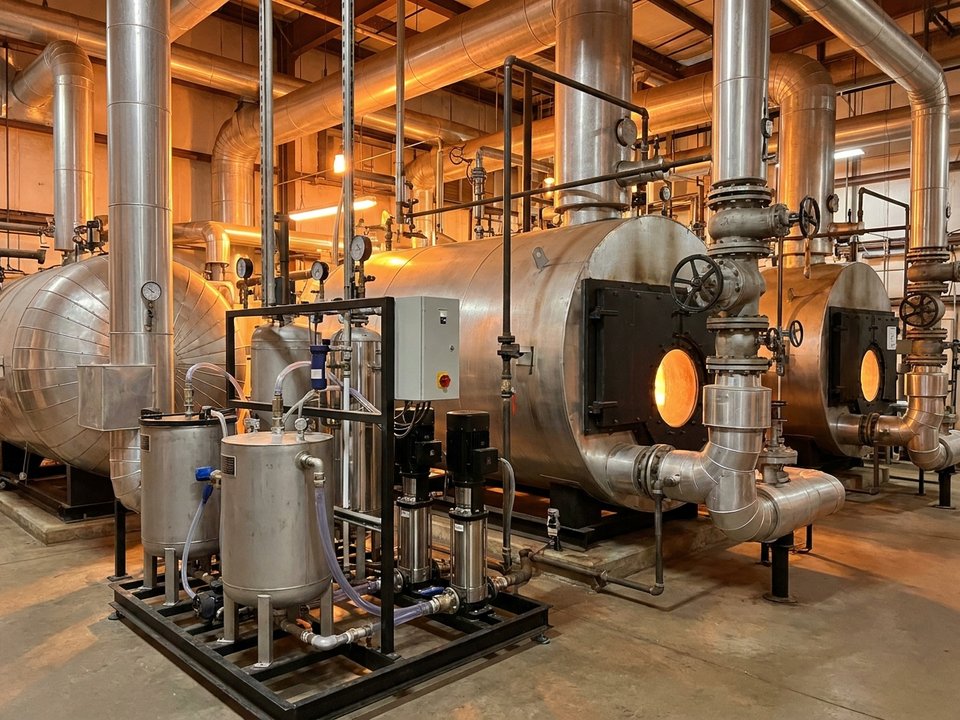
A boiler system's performance is directly dependent on the quality of the water inside it and the condition of the internal surfaces it heats. Scale formation on heat-transfer surfaces — even thin deposits — creates a measurable increase in energy consumption, as heat must conduct through an insulating mineral layer before reaching the process steam. Sludge accumulation settles and creates conditions for localised overheating and accelerated corrosion.
The result of unmanaged boiler-water chemistry is a system that becomes progressively less efficient, more expensive to operate and more prone to failure — often at the point where operational demand is highest.
Brykonchem's boiler-water treatment approach addresses feed-water conditioning, internal scale and corrosion inhibition, and sludge conditioning for effective blowdown management. Oxygen scavengers, alkalinity control, scale inhibitors and sludge dispersants are selected based on the boiler's operating pressure, feed-water characteristics, steam purity requirements and blowdown regime.
Effluent Water Treatment Solutions
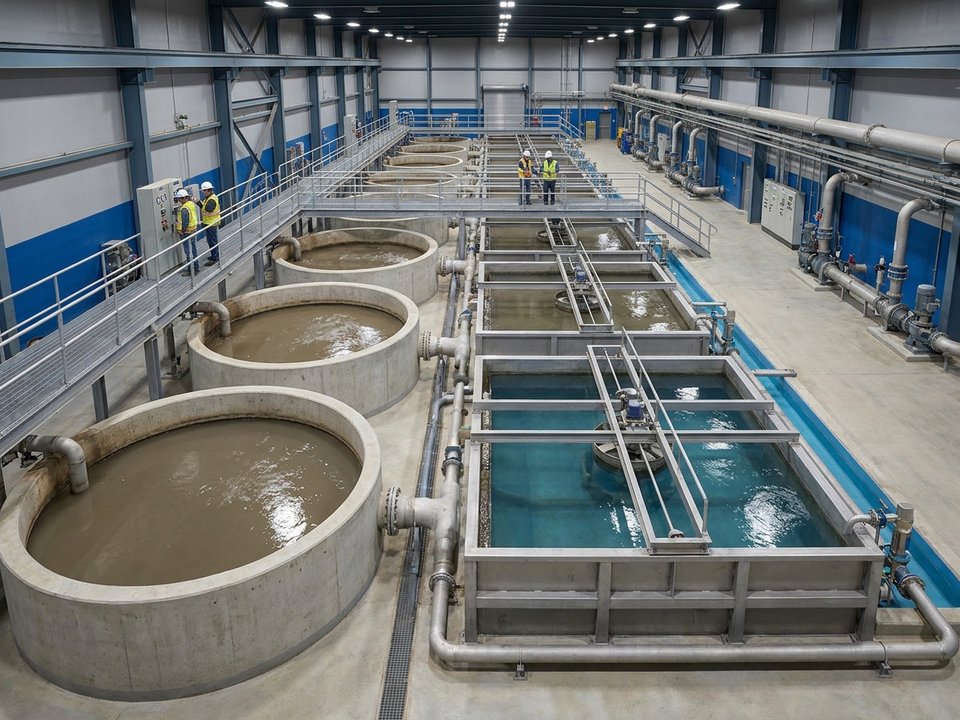
Industrial manufacturing generates wastewater streams that must be treated before discharge. The composition of these streams varies considerably by industry and process — from high-organic-load effluent in food and dairy operations to chemically complex streams from process industries — and the treatment approach must be matched to the specific characteristics of each effluent.
Regulatory discharge standards define the parameters within which treated effluent must fall. Non-compliance carries operational, financial and reputational consequences. But compliance alone is not the only objective: treatment efficiency, chemical consumption, sludge generation and process reliability all affect the total cost of running an effluent treatment plant.
Brykonchem supports industrial effluent treatment through application-focused chemistry selection. Coagulants and flocculants are matched to the suspended-solid and colloidal content of the stream. pH correction, biological support chemistry and disinfection are considered as part of an integrated treatment sequence.
Hygiene & Sanitation Solutions
In food processing, dairy and beverage environments, sanitation is a regulatory requirement and a production-quality control. Microbial contamination on surfaces, equipment and in the wider facility environment is not only a food-safety risk — it is a direct threat to product integrity and brand confidence.
Effective sanitation depends on more than applying a disinfectant to a surface. Contact time, concentration, surface condition, soil load, water hardness and the specific microbial populations present all affect whether a sanitiser achieves the required kill.
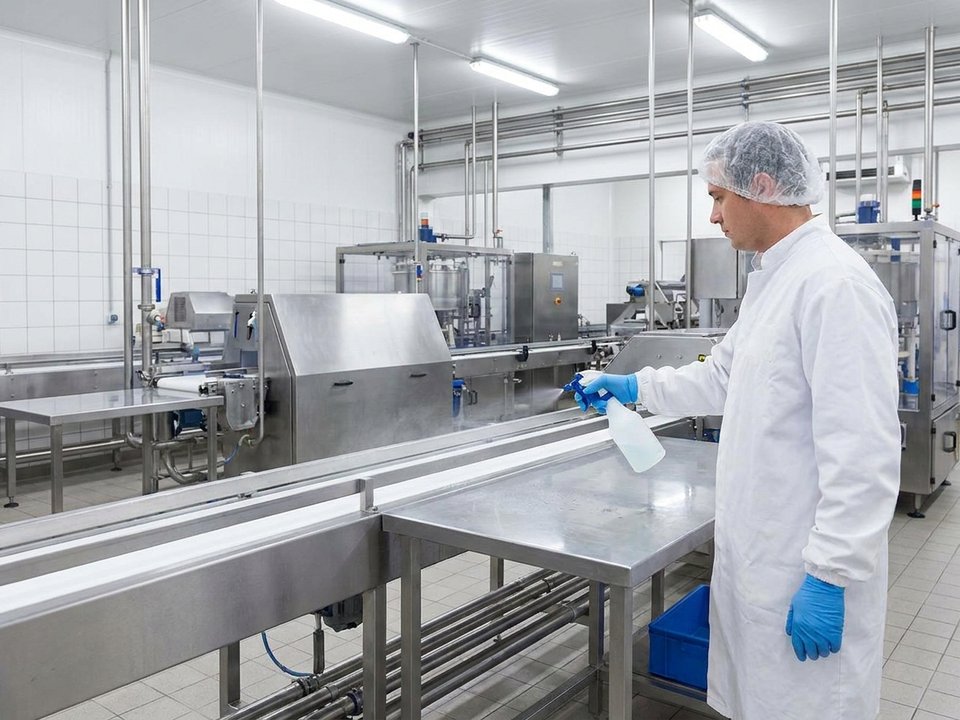
Brykonchem's hygiene and sanitation chemistry covers surface disinfection for food-contact and non-food-contact surfaces, equipment sanitation within CIP and clean-out-of-place (COP) protocols, and hand hygiene for food-handling environments. Product selection is guided by the surface type, the microbial risk profile, the regulatory requirements of the operating environment and compatibility with the existing cleaning programme.
Custom Formulations and Tailored Process Solutions
Not every process challenge fits a standard chemistry range. Operating conditions vary — feed-water composition differs between sites, equipment design imposes constraints, sustainability objectives shape chemistry selection, and some applications involve combinations of fouling types or process conditions that require a formulation developed specifically for the task.
Brykonchem's custom formulation capability is grounded in the same application-focused methodology that underpins all our work. Before any formulation is evaluated or developed, we examine the process conditions in detail: the nature of the challenge, the equipment involved, the water characteristics, the temperature and contact-time parameters, the compatibility requirements with other chemistry in use, and any sustainability or regulatory constraints that apply.
From this analysis, we identify whether an existing formulation can be adapted, whether a new combination of actives and carriers is required, or whether the solution lies in optimising the application protocol. The objective throughout is a solution that performs in your specific conditions — not a compromise between your requirements and what happens to be available in a standard catalogue.
Industries We Serve
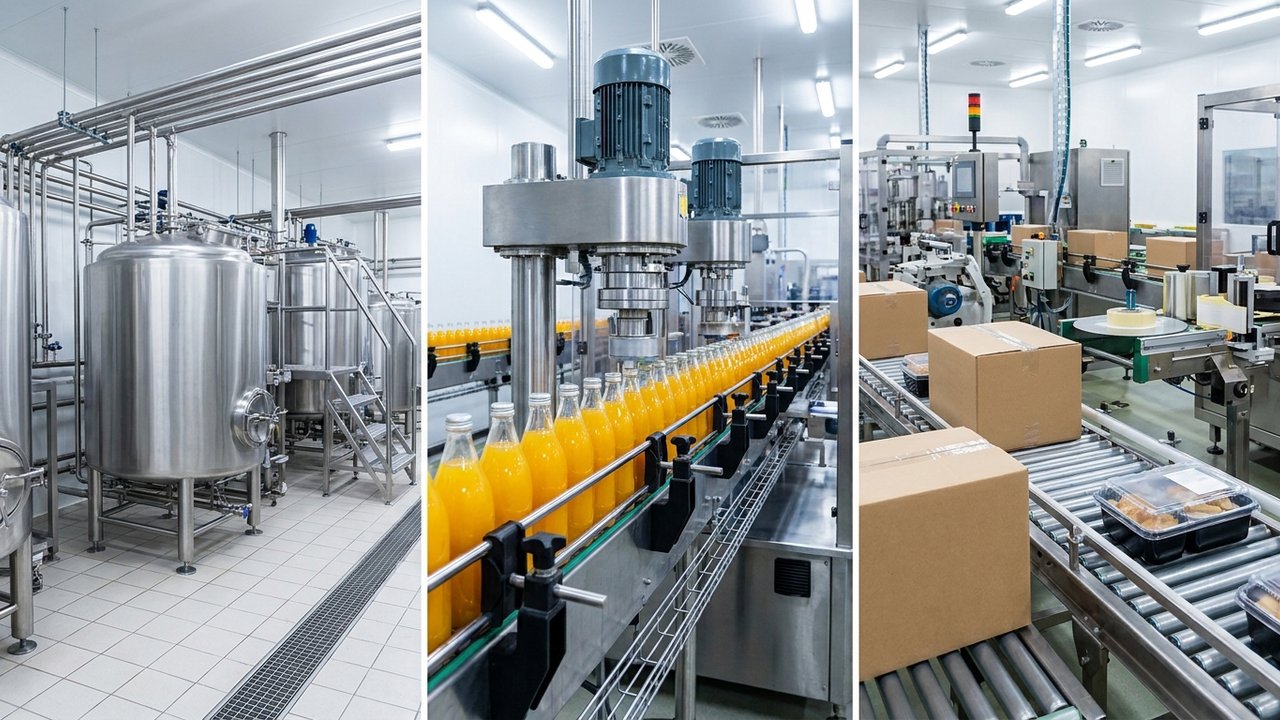
Brykonchem works with manufacturers and industrial operators across sectors where cleaning performance, hygiene reliability and water-system efficiency are operationally critical. Each industry presents distinct chemistry and application requirements — and we approach each with the specificity those requirements demand.
Food Processing
Food manufacturing environments require cleaning and sanitation programmes that meet food-safety standards while managing the wide range of soils generated by processing — proteins, fats, starches, sugars and combined residues. Downtime for cleaning must be minimised without compromising hygiene assurance.
Dairy Industry
Dairy applications involve some of the most chemically demanding CIP cleaning requirements — heat-denatured proteins, milk stone mineral deposits and fat residues that require carefully sequenced alkali-acid cleaning programmes. Hygiene standards are non-negotiable in environments producing food for direct consumption.
Beverage Industry
Beverage producers face sanitation and cleaning challenges across a wide range of process environments — from high-sugar liquid-food lines to carbonated beverage filling and packaging. Consistent sanitation and clean-equipment protocols are central to product quality and regulatory compliance.
Process Industries
Industrial process operators rely on reliable cooling-water treatment, boiler chemistry, membrane performance and effluent management to maintain production continuity. Equipment protection and regulatory compliance are the primary drivers of chemistry selection in these environments.
Facility Management
Managed-facility operators require professional cleaning and hygiene chemistry for surface sanitation, washroom hygiene and general facility maintenance — with product performance that is reliable and practical across the scale of managed environments.
Hospitality
Hotels and commercial hospitality environments require cleaning and sanitation products that meet hygiene standards across kitchens, guest areas and laundry operations — where reliability, surface compatibility and safety-in-use are all important considerations.
Why Manufacturers Choose Brykonchem
The difference between a chemical supplier and a technical process-performance partner is the depth of understanding brought to each engagement. Brykonchem is built around the latter.
Application-Focused Expertise
Our solutions are developed around real-world cleaning, hygiene, membrane and water-treatment challenges — not around a product range that needs selling. The application comes first; the chemistry follows from it.
Performance-Driven Chemistry
Formulations are engineered to support cleaning efficiency, process reliability and consistent operational performance. We measure success by what happens in your process, not by volume supplied.
Industry-Specific Solutions
Food, dairy, beverage and industrial environments each present distinct chemistry and application requirements. Our solutions are aligned to the specific demands of each sector, not adapted from a generic range.
Responsive Technical Support
Technical support extends through the full engagement — from initial solution selection through implementation, optimisation and ongoing performance improvement. When process conditions change, the support continues.
Problem-First Methodology
Every engagement begins with understanding the process challenge. We do not prescribe chemistry before understanding the system it will operate in. This discipline produces recommendations that perform.
Integrated System Thinking
Soil type, water quality, chemical selection, concentration, temperature, contact time and mechanical action are not independent variables. We treat them as an integrated system — because in practice, they are.
Custom Formulation Capability
Where standard chemistries do not match the process conditions, sustainability goals or equipment constraints of your application, we have the capability to evaluate and tailor formulations to your requirements.
A Trusted Technical Partner for Food, Dairy, Beverage and Industrial Sectors
Brykonchem is positioned as a specialised manufacturer of cleaning, hygiene and water-treatment solutions for food, dairy, beverage and industrial manufacturing environments. Our focus on application-led chemistry — rather than catalogue supply — is what manufacturers in these sectors rely on when they need process performance they can depend on.
We work with plant managers, process engineers, operations teams and facility managers who need a chemistry partner that understands their process, not one that simply fulfils a purchase order.
Start With Your Process Challenge
Whether you are experiencing membrane fouling, struggling with CIP cycle performance, managing a cooling-water or boiler chemistry problem, dealing with effluent compliance, or looking for hygiene solutions matched to your operating environment — the starting point is a conversation about what is actually happening in your process.
Brykonchem's technical team is available to discuss your challenge, assess what information is needed, and outline an application-focused approach to addressing it. There is no obligation to purchase — the conversation is about understanding your process first.
Reach Us Directly
You can reach us to discuss your process challenge, request a quote for a specific chemistry requirement, or contact our technical team directly.